
SOLUTION
Production lines for the heavy clay industry
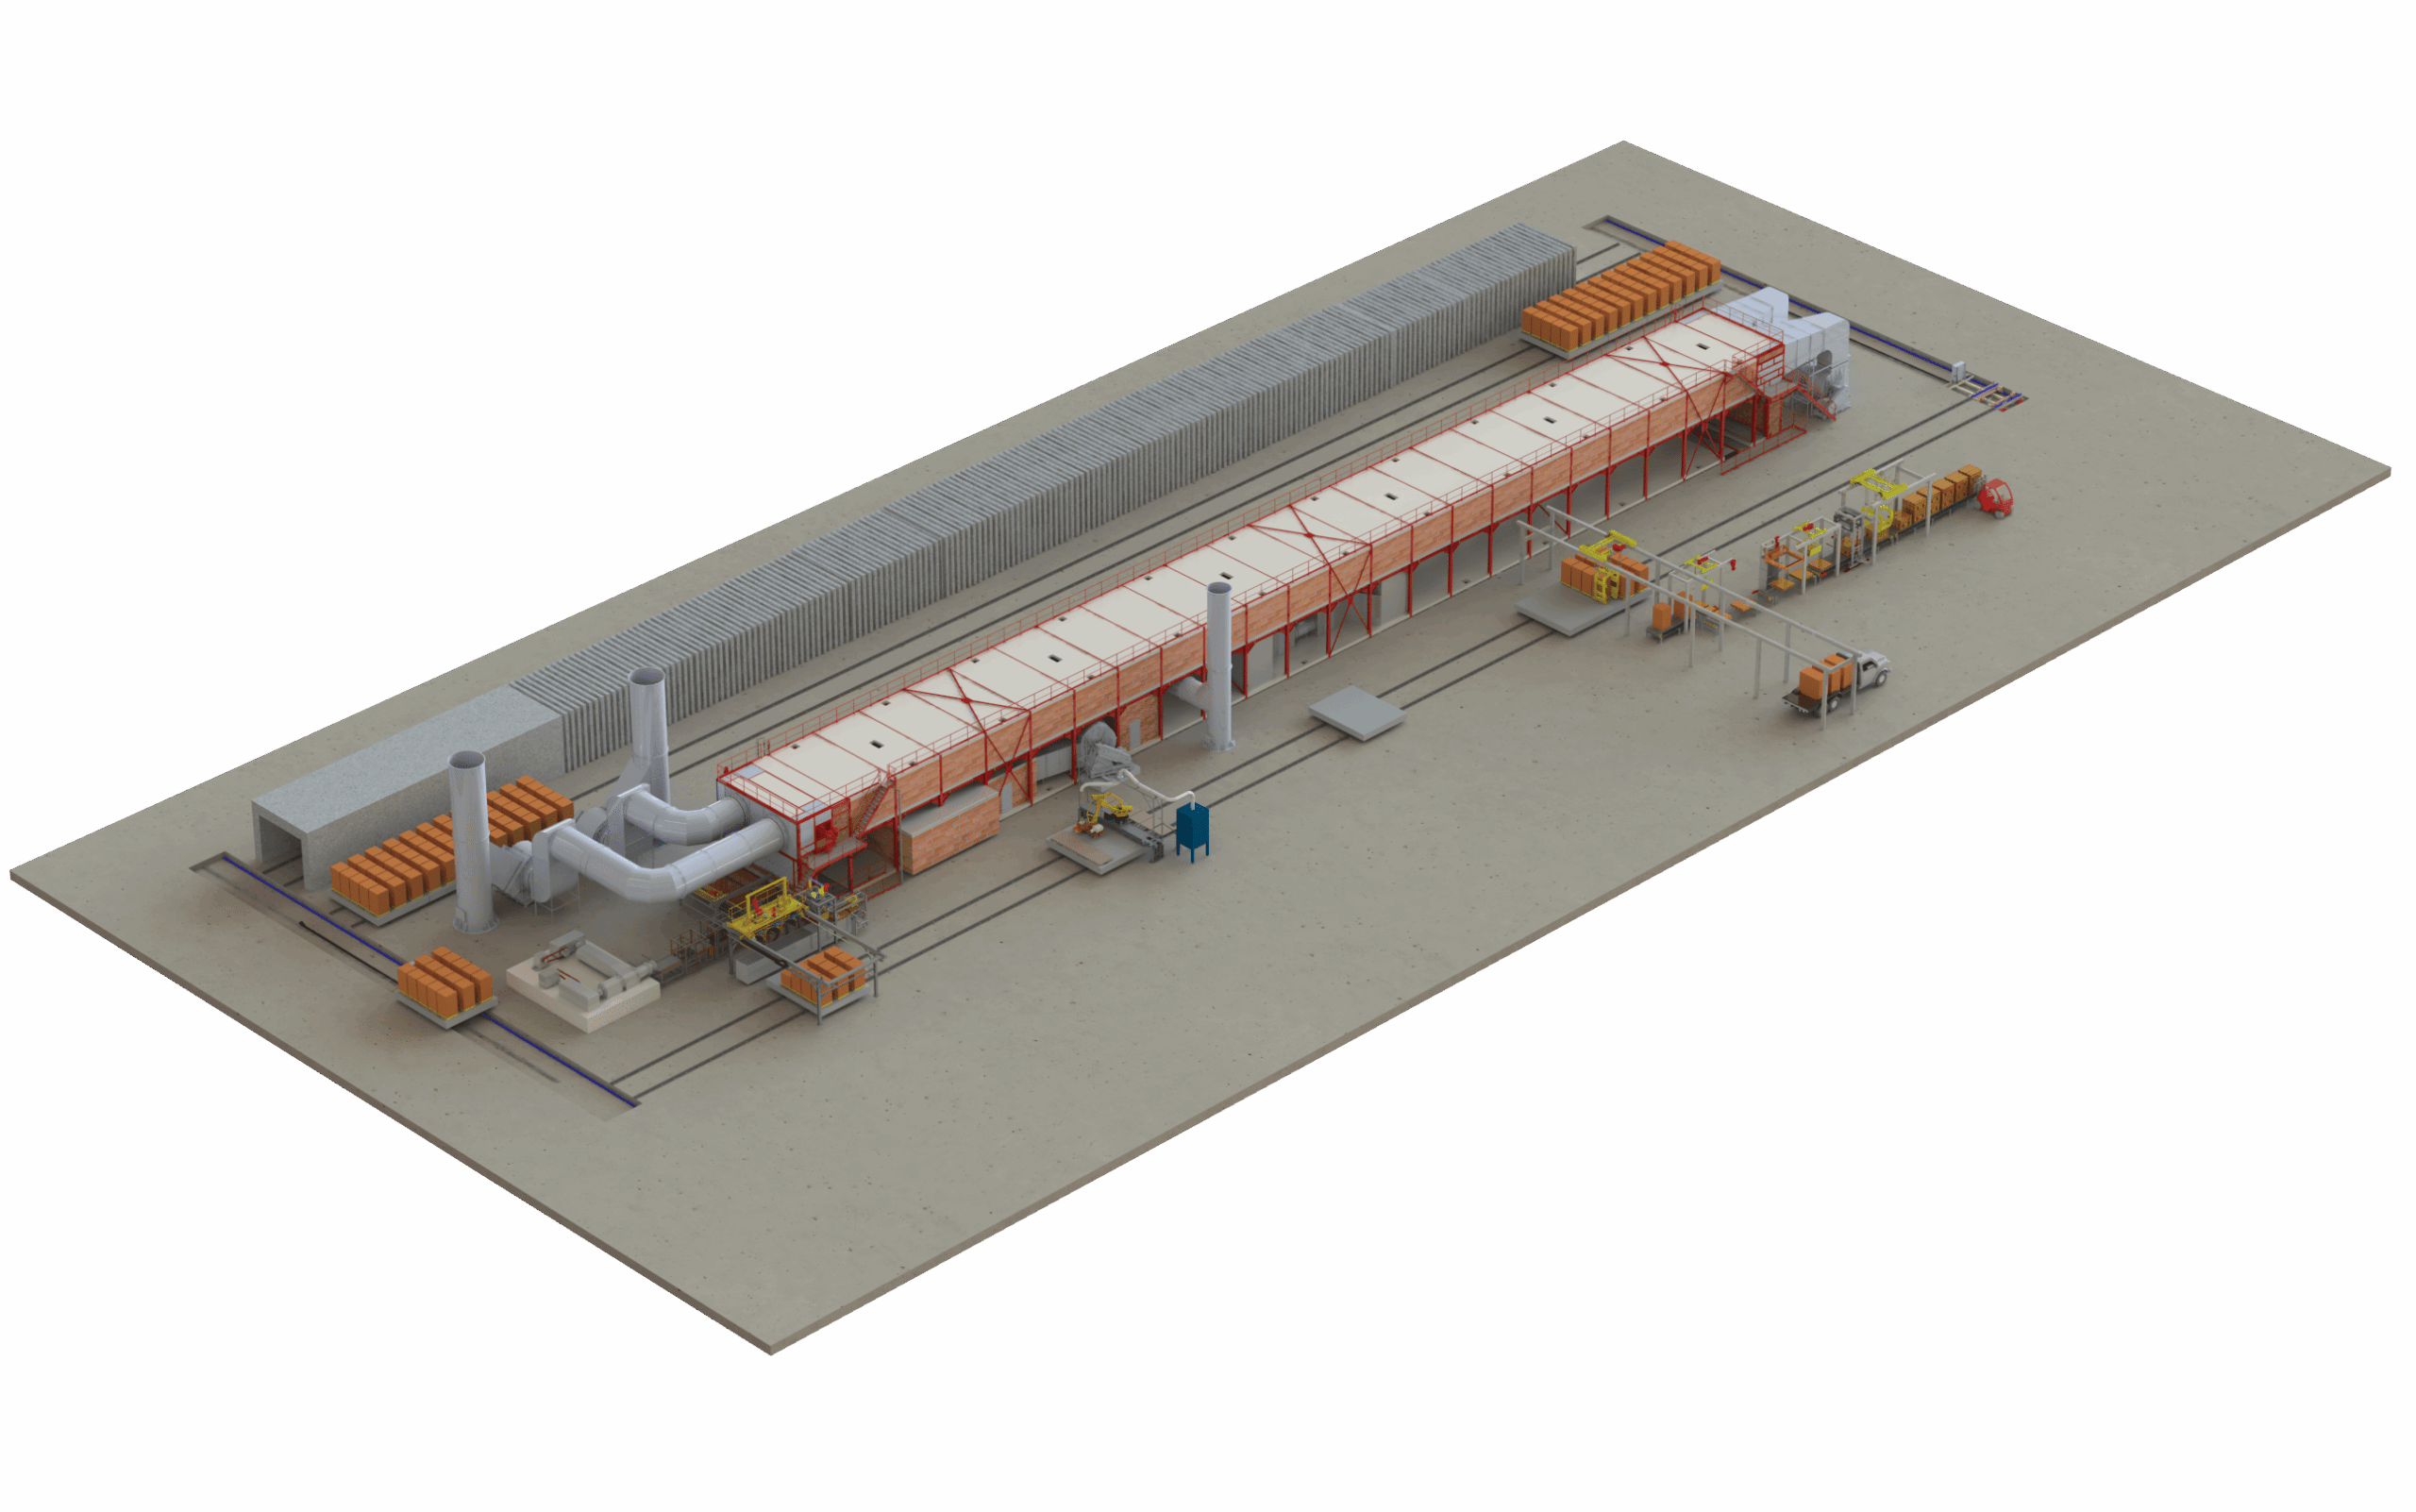
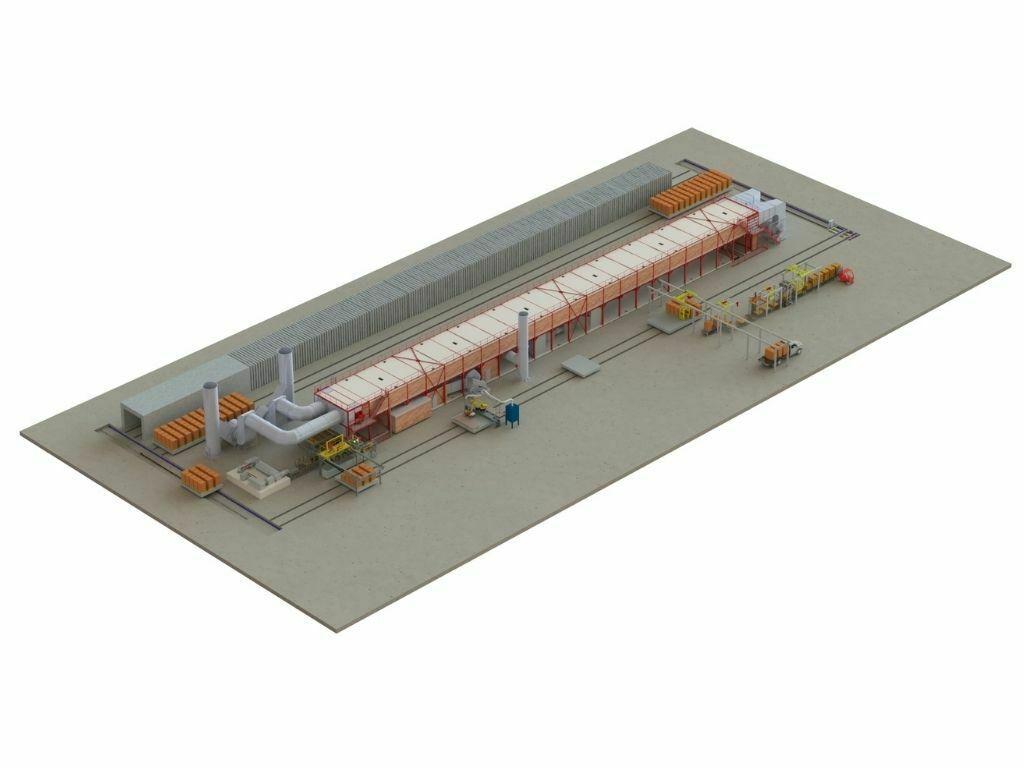
FIMEC SH integrates cutting and handling equipment into brick and roof tile production lines. The equipment feeds dryers, loads and moves kiln cars, then unloads fired products for pack formation.
Products
Bricks, roof tiles, blocks and pavers
Dryers
ANJOU APO carrier loading
Kiln cars
Stacking lengthways or across the car
Packing
One or more lines after unloading
Cutter
Independent cylinder-tensioned wires
From the cutter to finished brick packs
Products change supports during drying and firing. The handling system coordinates these transfers: feeding dryer carriers, loading kiln cars, moving cars between stations and unloading after firing.
Brick arrangement on the kiln car prepares the load for the kiln. The stacker can space products during placement or build staggered layers. After firing, unloading supplies either pack collection or a packing line.
Line functions
High-capacity cutter arrangement
Six 300 mm products lengthways, eight across
Clay crushers
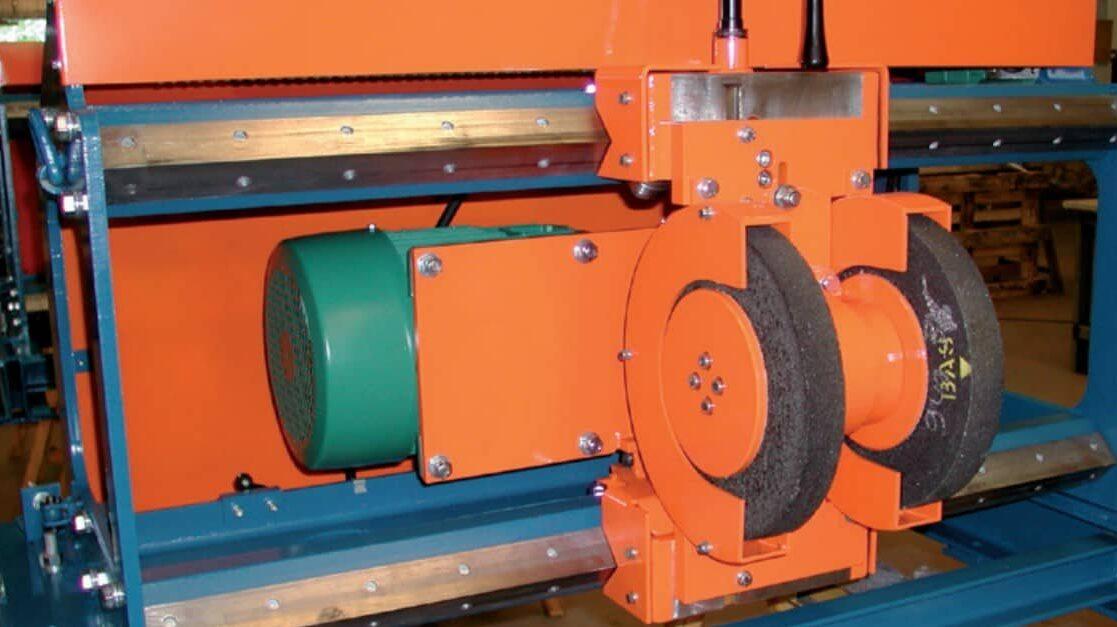
Roll grinding with two grinding wheels
Crosswise stacking
Up to eight independent grippers
Layer arrangement
Product spacing and staggered placement available
Transfer cars
Layout matched to existing civil works
Cleaning
Vacuum removal of dust and broken material
Fired product discharge
One or more packing lines
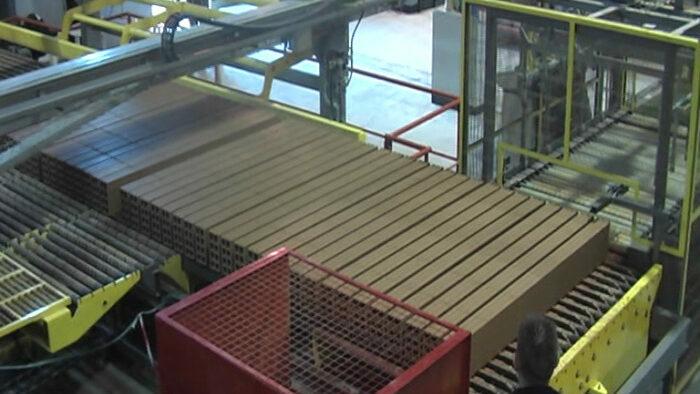
The cutters handle bricks, extruded roof tiles, blocks and pavers. The high-capacity cutter uses independent wires, each tensioned by its own cylinder. One configuration accommodates six 300 mm products lengthways and eight across.
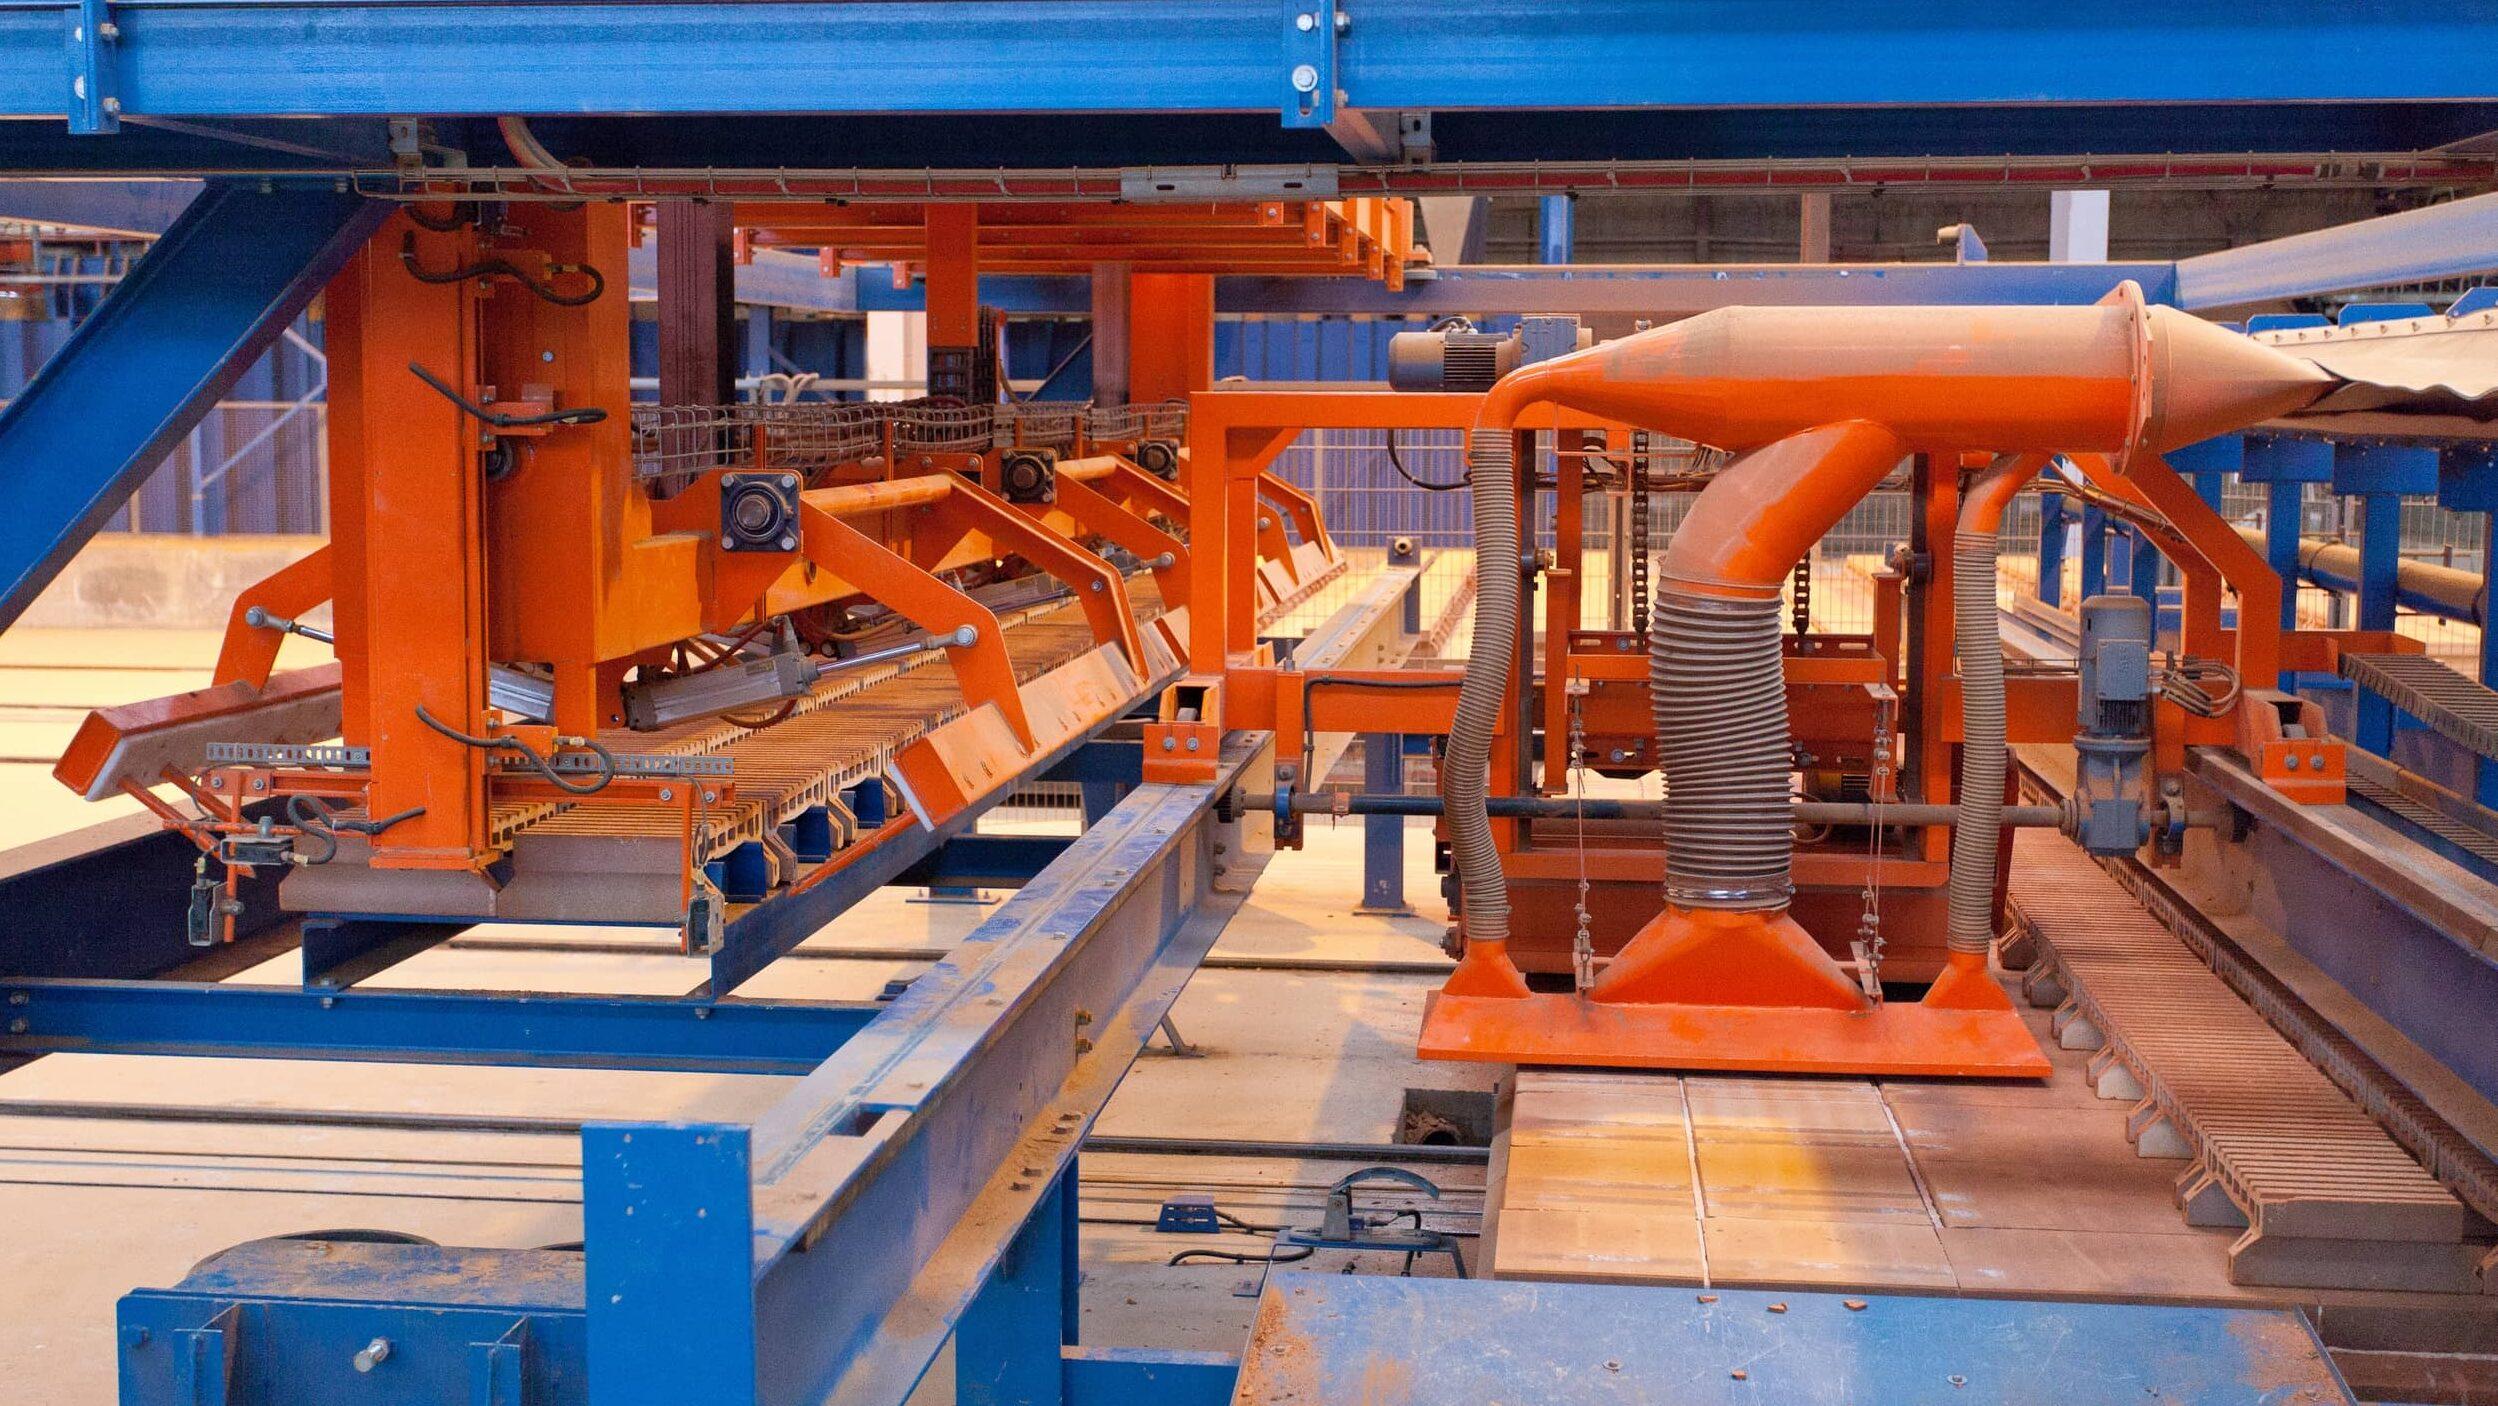
Loaders place products on the carriers of the ANJOU APO dryer. Carrier width and structure determine the loading arrangement. Twin-wheel grinding machines also serve clay preparation by grinding the crusher rolls.
Loading can run along the kiln car or across it. The crosswise arrangement can include up to eight independent grippers handling several product layers.
Transfer cars and handling carts move kiln cars between tracks and stations. Their layout takes account of the tracks and the depth of existing civil works. Wheels and lubrication units are separate components of this handling system.
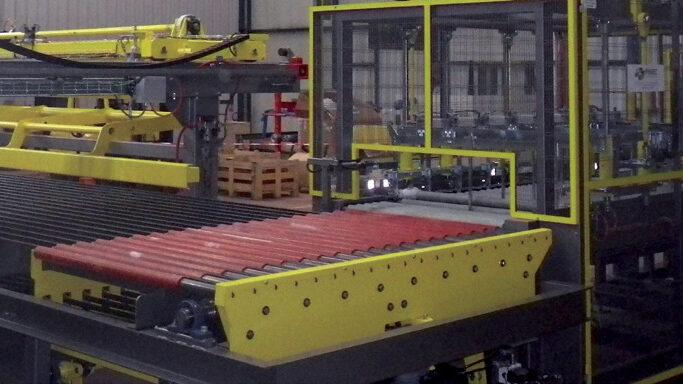
The unloader directs products to one or more packing lines. Grippers form the fork openings directly in the packs, limiting brick travel on roller conveyors.
Before the next loading cycle, the cleaner removes dust and broken material from the top of the kiln car and beneath the deck slabs. Repositioning refractory components can supplement cleaning. See the kiln car cleaner for details.
Equipment used in this solution
Equipment
Wheels and lubrication units for industrial cars
Wheels and lubrication units equip kiln cars, dryer cars and transfer cars. The wheels use forged steel with hardened treads and flanges; automatic lubrication operates as the car passes.
Equipment
Robotic kiln car cleaners
The kiln car cleaner removes dust and broken material from the top of the car and beneath the deck slabs. The robotic version can include a refractory component repositioning function.
Equipment
ANJOU dryers for heavy clay
The ANJOU APO carrier dryer is part of Alfi Fimec’s industrial heritage. Its optimised-pitch principle reduces spacing between carriers inside the dryer. FIMEC SH supports this equipment, including mechanical refurbishment, ventilation and burner work.